
Pendulum Bucket Z Elevator for Gentle Product Handling
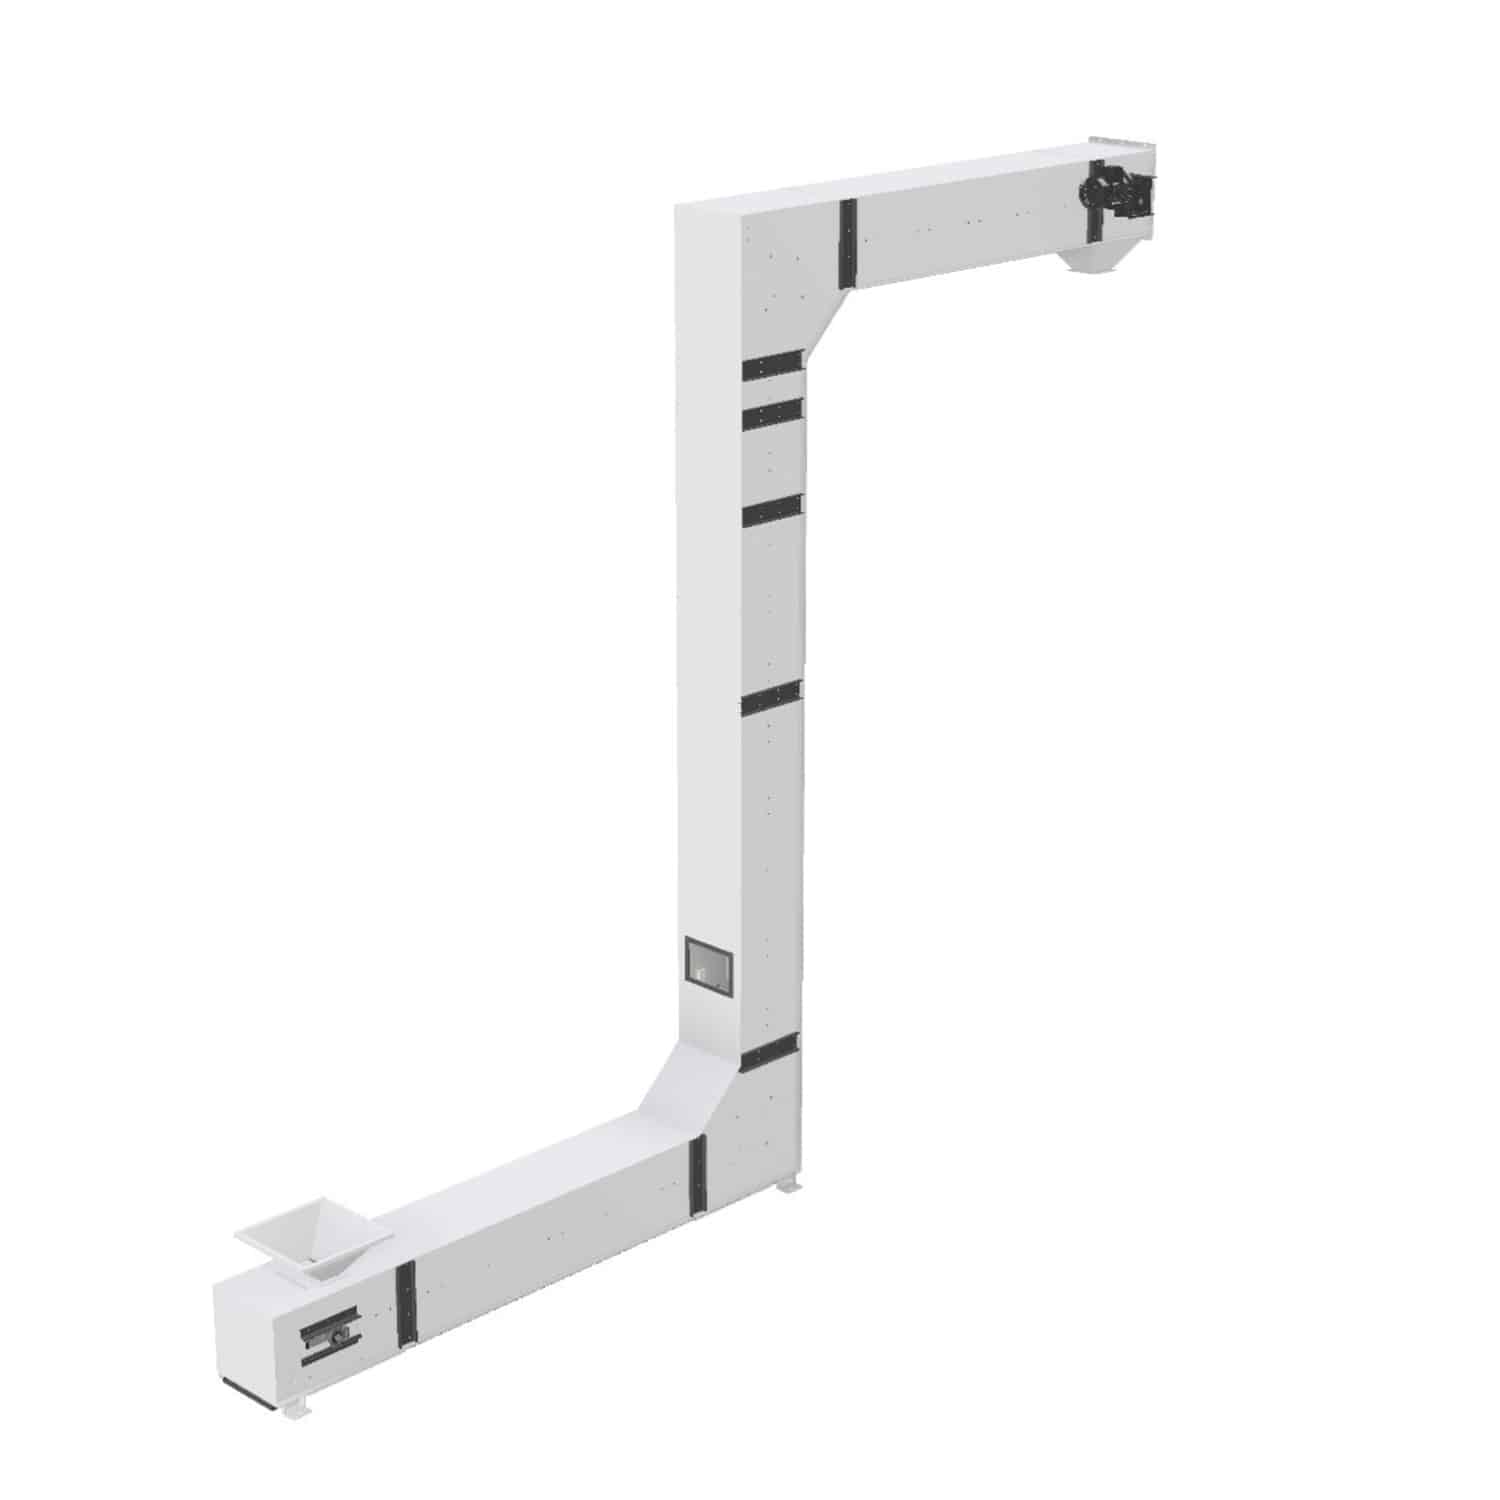
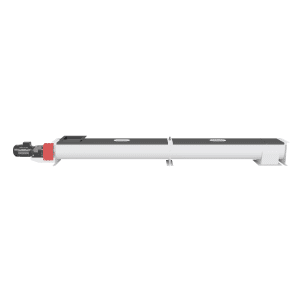
The ADDAMS Pendulum Bucket Z Elevator is a continuous conveying system for lifting and transferring grain, seed, pulses, nuts, food ingredients and other free-flowing bulk products. Its linked buckets travel through horizontal, vertical and upper horizontal sections, allowing one machine to receive product at a low level, elevate it and discharge at one or more selected positions.
The pendulum bucket arrangement helps the buckets remain upright while travelling through the conveyor path. Product is carried inside the buckets rather than dragged through a casing or pushed by a screw. This operating principle can support gentle handling, compact layouts and flexible discharge arrangements when the machine is correctly selected for the material and duty.
Typical Applications
- Feeding optical sorters, multihead weighers and packaging machines
- Lifting seeds, pulses, nuts, snacks, granules and similar products
- Connecting processing equipment where vertical and horizontal transfer are both required
- Distributing one product to several bins or downstream machines
- Moving fragile or high-value materials with controlled transfer points
- Serving food, seed and agricultural plants with frequent product changes
How the Pendulum Bucket System Works
Product enters the lower loading section and is directed into a sequence of overlapping or closely spaced buckets. A chain or linked carrier system moves the buckets along the horizontal inlet section, around the lower corner, upward through the vertical casing and then across the upper horizontal section.
At the selected discharge, the bucket is guided or tipped so the product leaves under controlled conditions. The empty bucket then returns through the machine to repeat the cycle. The loading rate, bucket filling, conveyor speed and discharge timing must work together so product does not spill, accumulate or overload the drive.
Main Components and Design Functions
| Component | Function | Selection Considerations |
|---|---|---|
| Pendulum buckets | Carry product through horizontal and vertical sections | Volume, product contact material, overlap, cleanability and impact resistance |
| Chain or carrier system | Moves and supports the buckets | Conveyor length, load, speed, duty cycle and wear |
| Lower loading section | Receives product and fills the buckets | Feed control, drop height, product distribution and spill prevention |
| Vertical casing | Encloses and supports the lifting section | Lift height, access, dust containment and structural support |
| Corner and guide sections | Direct bucket travel through changes in direction | Geometry, chain tension, bucket clearance and maintenance access |
| Discharge station | Releases product to the selected destination | Position, chute geometry, actuation and residual-product control |
| Motor and gearbox | Provide controlled conveying power | Bucket load, route length, lift height, starts and safety margin |
| Controls and sensors | Coordinate operation and monitor faults | Interlocks, speed monitoring, level sensing and destination selection |
Capacity and Elevator Selection
Required throughput is established from usable bucket volume, bucket spacing, operating speed, product bulk density and the achievable filling level. The practical capacity may be limited by the inlet, discharge station or downstream equipment rather than the carrying section alone. Product condition can also change its filling behavior.
Gentle Handling and Product Protection
Because the product is carried inside individual buckets, the system can reduce continuous rubbing and mechanical pushing. Low-speed operation and well-designed loading and discharge transitions may help protect seed, nuts, snacks and coated products. However, no mechanical conveying system is completely damage-free.
Product can still experience impact at the inlet, between particles inside the bucket and at the outlet. Representative testing is recommended when a defined breakage, coating-loss or appearance limit is required. Drop heights, chute angles, bucket filling and downstream transitions should be considered as one product-handling route.
Z, C and Custom Conveyor Routes
The familiar Z arrangement combines a lower horizontal section, vertical lift and upper horizontal transfer. Depending on the machine design and plant space, other routes may also be possible, including C-type or extended configurations. The selected path should minimize unnecessary corners while reaching the required inlet and discharge points.
Multiple Inlets and Discharge Points
A pendulum bucket elevator can be configured to collect product from selected feed points or distribute it to several destinations. This is useful above packaging lines, storage bins or process machines. The operating logic must ensure that the correct discharge is active before product reaches it.
Feeding and Loading Control
The inlet should provide a stable flow matched to bucket capacity. Uncontrolled surges can overfill buckets, create spillage and increase load on the drive. A vibratory feeder, belt feeder, screw feeder, gate or buffer hopper may be used when the upstream machine cannot deliver a consistent rate.
Loading geometry should distribute product into the bucket without excessive free fall. The feed chute must remain clear of the moving buckets and should not create ledges where material can collect. Interlocks should stop upstream flow if the elevator stops or a high-level condition is detected.
Hygiene, Cleaning and Cross-Contamination
Buckets and product-contact surfaces may be manufactured from materials selected for the process. Food or seed applications can require specific bucket materials, surface finishes, seals and cleaning methods. A general material description alone does not establish compliance with every hygiene standard.
Access doors, removable panels and clean-out points can support inspection, but residues may remain in buckets, corners, guides and discharge chutes. Plants handling allergens, different varieties or treated seed should use a validated cleaning procedure. Where frequent changeover is critical, the required access and cleaning time should be agreed before final design.
Dust Control and Enclosure
An enclosed casing helps contain product, although dust may escape at loading, discharge and ventilation points. Dust connections can be provided where required and should be coordinated with the plant aspiration system. Excessive extraction may remove light product or disturb bucket filling, so airflow must be balanced for the duty.
Controls and Safety
The elevator control system may include motor protection, speed or motion monitoring, chain-tension or misalignment supervision, level sensors and discharge-position feedback. Interlocking with upstream and downstream machines helps prevent overfilling and blocked chutes. A controlled starting method may be selected for the drive and plant electrical system.
Moving chains, sprockets, buckets and drive parts require appropriate guards and enclosure. Access doors should be opened only under an approved isolation and lockout procedure. Emergency stops, platforms and local safety devices are determined from the final installation and risk assessment.
Installation and Structural Integration
Accurate alignment is essential for smooth bucket travel and even wear. The supporting steelwork should control movement and provide stable points at the lower, vertical and upper sections. Tall installations may require intermediate supports or bracing developed for the site conditions.
Maintenance for Reliable Operation
Routine inspection should cover buckets, links or chains, guide components, sprockets, tensioning equipment, bearings, fasteners, guards and sensors. Cracked buckets, loose attachments, abnormal noise or changing bucket clearance should be investigated before continued operation. Chain elongation and guide wear should be recorded over time.
Cleaning and maintenance intervals depend on operating hours, product and environment. Product buildup should be removed before it interferes with bucket movement or discharge. A documented preventive-maintenance plan helps schedule wear-part replacement and reduce unexpected stoppages.
Frequently Asked Questions
What products can a Pendulum Bucket Z Elevator handle?
It can handle many free-flowing seeds, grains, pulses, nuts, snacks, pellets and granules. Suitability is confirmed from the product properties, hygiene needs and operating duty.
Is the elevator suitable for fragile products?
It can provide controlled handling because product is carried in buckets. Representative trials are advisable when a specific damage or appearance limit must be achieved.
Can the system discharge to several machines?
Yes. Multiple discharge stations may be engineered, with sensors and control logic used to select the correct destination and prevent unintended mixing.
Can it follow a route other than a Z shape?
Alternative routes may be possible depending on the machine design and available space. ADDAMS confirms the practical geometry from the plant layout and process interfaces.
How is elevator capacity determined?
Capacity depends on bucket volume, spacing, speed, filling level, bulk density, lift and discharge limitations. Project assumptions are stated in the technical proposal.
How is the elevator cleaned?
Cleaning uses accessible buckets, covers, inspection points and approved procedures appropriate to the product. The required changeover and hygiene standard should be defined before design.
Request a Project-Specific Proposal
Send ADDAMS your product details, required capacity, lift height, horizontal distances, inlet and discharge positions, operating hours and hygiene requirements. Our team can configure a Pendulum Bucket Z Elevator and connected equipment for your processing, storage or packaging line.
Related Equipment and Process Options
Compare transfer arrangements using the route, discharge points, product sample and required handling conditions.
- Grain Bucket Elevator for Seeds & Cereals
- Continuous Cup Bucket Elevators
- Easy Dump Bucket Elevator
- Grain & Seed Belt Conveyor Systems
- Fine Seed Cleaners
Share your product sample, target capacity, quality requirements and existing line layout. Request your custom quote from ADDAMS to evaluate equipment selection and process connections.
Reviews
There are no reviews yet.